How to Choose a Regenerative Thermal Oxidizer
Choosing a Regenerative Thermal Oxidizer is a practical engineering decision, not a contest to find the highest advertised destruction efficiency. The right system must match the exhaust stream, operating schedule, and site constraints. A unit sized for the wrong flow can waste fuel, struggle with temperature swings, or require costly changes later.
Start with measured process data. Record normal and peak airflow, contaminant types, concentration ranges, moisture, and temperature. Note whether production runs continuously or in batches. These details shape chamber design, heat recovery, burner demand, and valve selection. Small differences matter. A coating line that surges during product changes may need a different operating strategy from a steady process.
This guide compares the factors that influence RTO selection: treatment performance, thermal efficiency, pressure drop, materials, controls, footprint, and maintenance access. It also explains what to ask suppliers and how to evaluate lifecycle costs alongside purchase price. Look closely at guarantees, assumptions, and service support.
One point needs care: no verified expert quotation or source material was provided for this request. Rather than invent a specialist’s name or words, this introduction avoids a false attribution. A trustworthy selection process deserves evidence, not a polished but unsupported quote. Before choosing a Regenerative Thermal Oxidizer, confirm that proposed performance claims reflect your actual operating conditions.
How a Regenerative Thermal Oxidizer Works
How to Choose a Regenerative Thermal Oxidizer
How a Regenerative Thermal Oxidizer Works
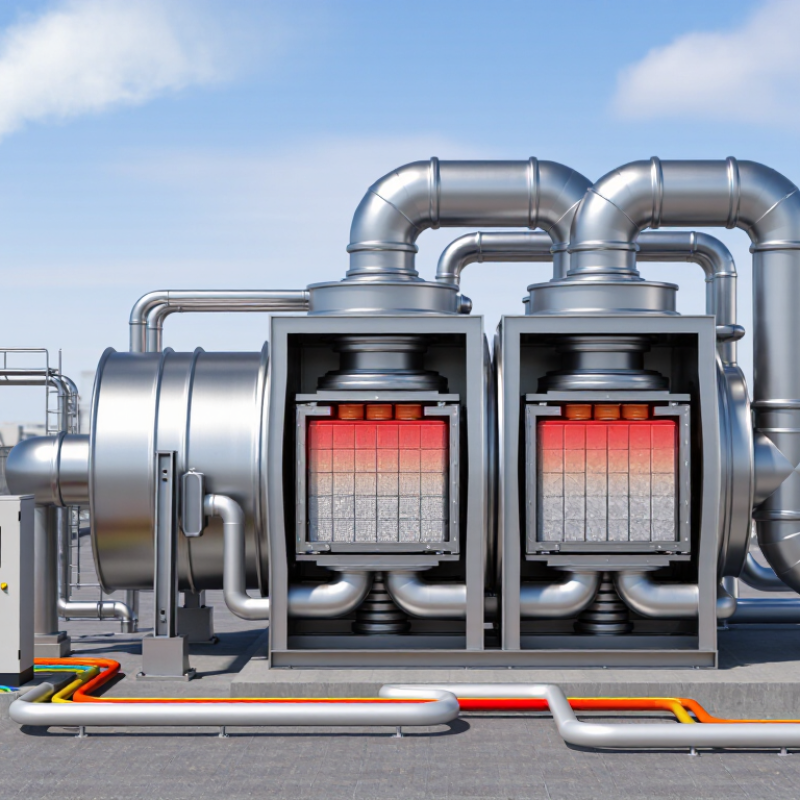
A regenerative thermal oxidizer destroys certain pollutants in industrial exhaust by exposing them to high temperatures. Inside the unit, a burner heats a combustion chamber. Exhaust passes through a ceramic bed, which absorbs heat from treated gas leaving the system. A switching valve then directs incoming exhaust through the warmed bed. This preheating reduces the fuel needed to reach operating temperature. The cleaned, hot gas transfers much of its remaining heat to another ceramic bed before exiting. Valves periodically reverse the flow, so the beds alternate between heating and storing heat.
Tips: Ask for performance data at your actual airflow, pollutant concentration, and operating schedule. Check how the unit handles startup, shutdown, and changing exhaust conditions. Inspect access points for ceramic media and valves; maintenance details matter. A design that looks efficient on paper may need adjustments in a real plant.
When choosing equipment, compare expected destruction efficiency, pressure drop, fuel use, and turndown range. Also consider whether the process produces sticky dust or compounds that could foul the beds. Request clear assumptions behind any energy estimates. Small changes in exhaust temperature can affect performance. And real operations are messy. Leave room for monitoring and tuning after installation, because actual plant conditions may not match the design case exactly.
How to Choose a Regenerative Thermal Oxidizer — How a Regenerative Thermal Oxidizer Works
An RTO destroys volatile organic compounds (VOCs) by heating contaminated air in a combustion chamber. Ceramic heat-transfer beds recover heat from treated exhaust and use it to preheat incoming process air. The figures below are general planning ranges; actual requirements depend on the gas composition, operating conditions, and applicable permit.
| Selection Dimension | What to Evaluate | Typical Planning Range or Consideration | Why It Matters |
|---|---|---|---|
| Exhaust airflow | Minimum, normal, and maximum flow; temperature; pressure; and expected variation during production. | Industrial systems commonly handle thousands to hundreds of thousands of standard cubic feet per minute (scfm); sizing must use the site’s measured design flow. | Undersizing can cause excessive pressure drop or inadequate treatment capacity; oversizing can increase capital and operating costs. |
| VOC concentration and composition | Identify each major compound, concentration range, variability, and any hazardous or corrosive constituents. | Concentrations are commonly expressed in parts per million by volume (ppmv) or milligrams per cubic metre (mg/m³). Compare the mixture with its lower explosive limit (LEL). | Composition affects destruction performance, supplemental fuel demand, materials selection, safety controls, and permit compliance. |
| Destruction performance | Required outlet limits, destruction and removal efficiency (DRE), test method, and permit conditions. | Many RTO designs are specified for approximately 95% or higher heat-recovery efficiency and high VOC DRE; required values are application- and permit-specific. | Performance guarantees should match the regulated compounds and the conditions under which compliance will be demonstrated. |
| Operating temperature and residence time | Determine the temperature and gas residence time needed for the target compounds and required destruction level. | Thermal oxidation often operates around 760–870°C (1,400–1,600°F), but the appropriate setpoint depends on the process gas and design. | Temperature and residence time affect destruction performance, fuel use, and thermal stress on equipment. |
| Heat recovery and fuel use | Review heat-recovery efficiency, startup fuel, steady-state support fuel, and expected operating hours. | Regenerative heat recovery can substantially reduce the energy needed to reheat incoming air. Actual fuel demand depends on VOC heating value, airflow, inlet temperature, and heat loss. | Energy performance is a major driver of lifecycle cost, particularly for systems that operate continuously. |
| Pressure drop and fan capacity | Check system pressure drop across ceramic media, ductwork, dampers, filters, and other process equipment. | Request pressure-drop data at minimum, normal, and maximum design airflow rather than relying on a single operating point. | Pressure drop determines fan power requirements and can affect the performance of upstream process ventilation. |
| Particulates, moisture, and contaminants | Assess dust loading, condensable compounds, water vapour, acids, and compounds that may foul or damage ceramic media. | There is no universal acceptable loading limit; pretreatment and media selection should be based on measured gas characteristics. | Fouling, corrosion, or plugging can increase pressure drop, reduce heat transfer, and require more frequent maintenance. |
| Safety and controls | Review LEL monitoring, purge sequences, flame safeguards, temperature interlocks, emergency shutdowns, and applicable codes. | Control and protection requirements depend on the process, fuel train, jurisdiction, and hazard assessment. | Appropriate safeguards help prevent unsafe mixtures and support reliable, compliant operation. |
| Turndown and production changes | Consider shifts, batch cycles, idle periods, changing airflow, and planned future production capacity. | Evaluate the full operating envelope, including startup, shutdown, low-flow, and peak-flow conditions. | A system suited only to normal production may operate inefficiently or require additional controls during off-design conditions. |
| Maintenance and lifecycle cost | Compare access to ceramic beds, valve and actuator maintenance, burner service, inspection needs, and spare-parts availability. | Include energy, maintenance, downtime, testing, and expected component replacement in lifecycle-cost estimates. | Purchase price alone does not show the long-term cost or operational reliability of an RTO. |